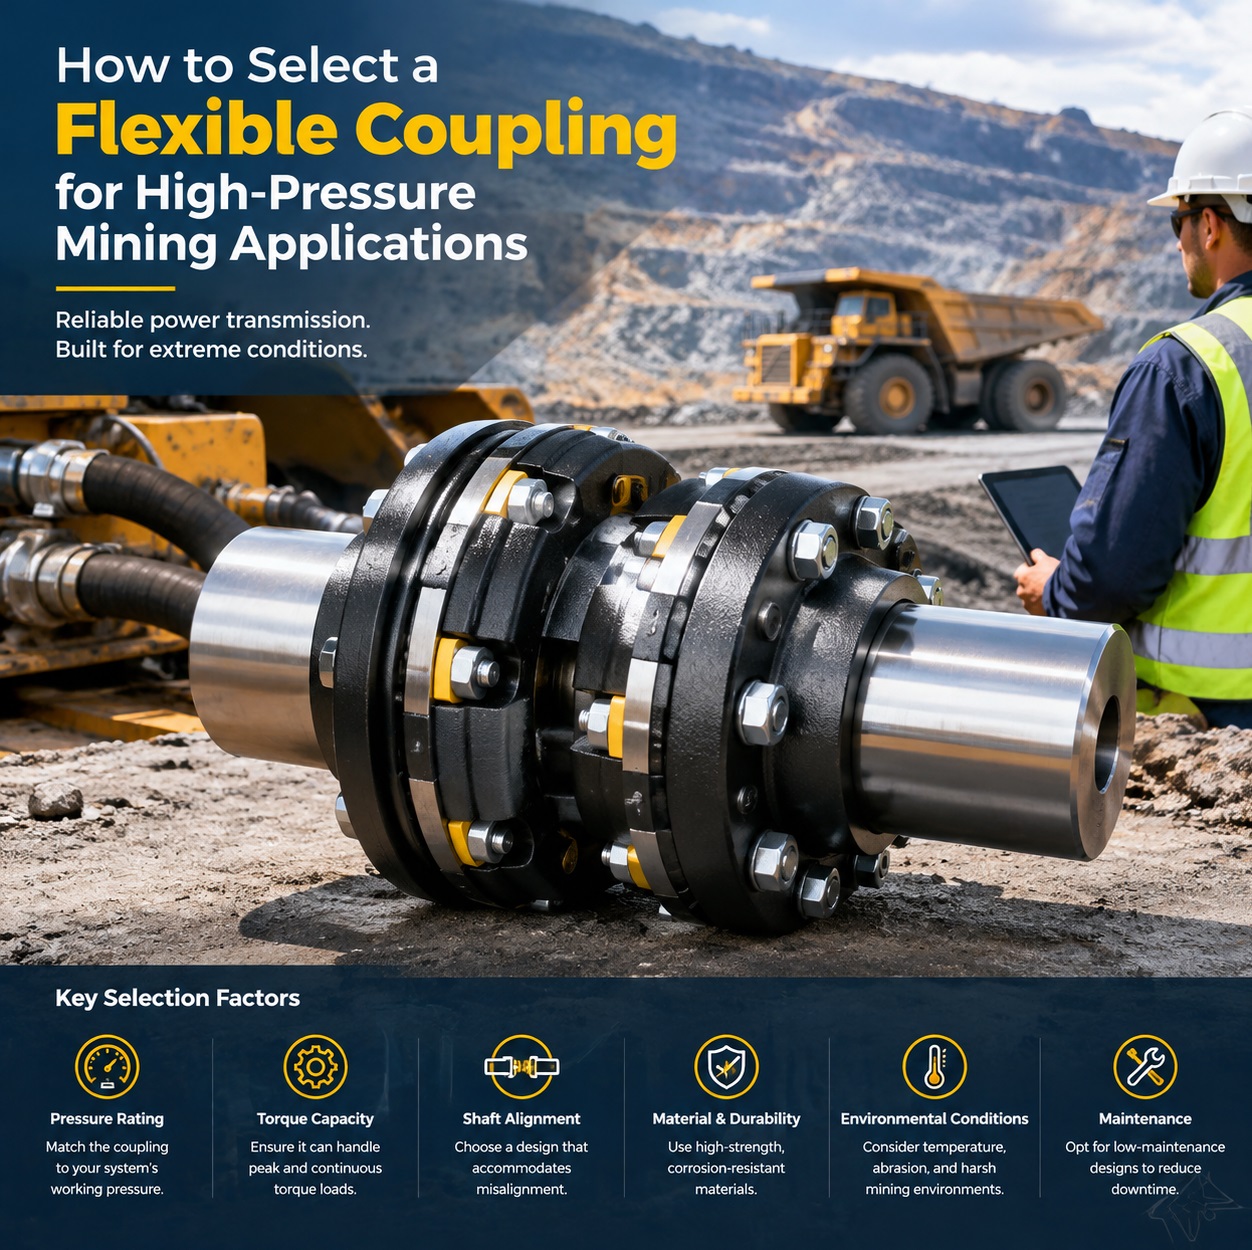
 A coupling that costs four hundred dollars can take down a plant that cost four hundred million. That ratio is why the selection process deserves more than a glance at a catalog page and a quick match on bore size.
Twenty-plus years of walking through mill buildings, pump houses, and conveyor transfer stations has taught me one thing about couplings in mining: they almost never fail because someone picked the wrong brand. They fail because someone sized them for the wrong reality. High-pressure duty, abrasive slurry, 24/7 operation, and maintenance crews stretched thin are a combination that punishes every optimistic assumption baked into the original selection.
So let’s strip this down to what actually matters when you’re specifying a flexible coupling for a high-pressure mining application.
START WITH THE TORQUE, NOT THE SHAFT
The first mistake is matching the coupling to the motor shaft diameter and calling it done. Shaft size tells you what fits. Torque tells you what survives.
You need to separate running torque from peak torque. A slurry pump moving high-pressure tailings might run comfortably at 1,200 Nm, then spike to three or four times that in a fraction of a second when a slug of coarse material hits the impeller. A crusher dealing with tramp metal, an apron feeder jamming on a chunk of rock, a conveyor starting fully loaded on an incline, all of these generate transient loads that dwarf the nameplate rating.
Mining service factors usually land between 1.5 and 2.0, but that range is a starting point, not a rule. Positive displacement pumps, reciprocating equipment, and drives with frequent starts push you higher. If the application has ever tripped a breaker or sheared a key, your service factor was too low. Size the coupling for the worst day the machine will ever have, not the average Tuesday.
MISALIGNMENT IS NOT A ONE-TIME PROBLEM
Every coupling in the plant was aligned perfectly on commissioning day. That alignment changes the moment foundations settle, pump casings heat up, or a pipe strain load shifts the housing a few thousandths of an inch.
You have three misalignment types to account for: angular, parallel, and axial. Most mechanical power transmission couplings handle some combination of all three, but the limits vary enormously. Elastomeric couplings forgive a lot of parallel and angular misalignment and absorb shock while they’re at it. Gear couplings handle high torque in a compact package but need continuous lubrication and tight alignment to survive. Disc couplings run clean, handle high speed and high torque with zero backlash, but they don’t damp vibration and they won’t tolerate much parallel offset.
Here’s the practical question: what will the alignment actually look like after two years of operation, not what does it look like on the alignment report? Design for that number.
THE ENVIRONMENT WILL FIND EVERY WEAKNESS
Mining environments are hostile in ways that bench testing never captures. Abrasive dust works its way past seals. Washdown water carries fines into every crevice. Process slurry coats everything within ten feet. Ambient temperatures swing from freezing to over 120 degrees Fahrenheit, and radiant heat from nearby equipment adds another layer.
This is where lubrication requirements become a decision point, not a detail. A gear coupling in a dry, clean, well-maintained drive train can run for decades. That same coupling in a slurry pump application with leaking seals will lose its lubricant, wear its teeth, and fail in months. If you can’t guarantee clean lubrication and regular inspection, choose a coupling that doesn’t need it. Elastomeric, disc, and grid couplings all offer lubrication-free options that hold up in dirty conditions.
Also check your elastomer compound. Standard nitrile is fine for many applications, but high-temperature service, ozone exposure, and certain chemicals demand EPDM, Viton, or a polyurethane element. The wrong compound turns hard and brittle long before its mechanical rating is reached.
TORSIONAL VIBRATION WILL EAT YOUR DRIVE TRAIN
High-pressure applications often involve variable frequency drives, reciprocating pumps, or diesel prime movers, all of which introduce torsional excitation into the system. If the excitation frequency lines up with a natural frequency of the connected equipment, you get resonance, and resonance destroys gearboxes, shafts, and couplings in short order.
Torsional stiffness of the coupling matters here. A very stiff coupling transmits vibration straight through. A softer coupling with good damping characteristics can shift the system away from a resonant condition and absorb the energy before it damages anything downstream.
For anything above a few hundred horsepower, or any drive with a reciprocating component, get a torsional vibration analysis before you commit to a coupling. It’s cheap insurance compared to replacing a gearbox.
THINK ABOUT FAILURE BEFORE IT HAPPENS
Ask yourself what happens when the coupling element wears out. Does it fail gradually with visible warning, or does it let go without notice? Can a maintenance tech replace the element in place, or does the drive need to be moved?
Spacer couplings exist for exactly this reason. On a high-pressure pump where the motor and pump are close-coupled, a spacer design lets you pull the element and even service the pump seal without touching the motor alignment. That single feature can turn a two-day job into a four-hour job.
Consider torque-limiting or shear-pin designs if the cost of a jammed or overloaded drive is catastrophic. Sometimes the smartest engineering decision is deciding what breaks first, and making sure it’s the cheap part.
THE BORING DETAILS THAT SINK INSTALLATIONS
Bore tolerance, keyway fit, hub clamping method, balance grade, and axial float all matter more than most people want to admit. Taper-lock and shrink-disc hubs transmit more torque on smaller shafts than a straight keyed bore, and they’re easier to remove after years of service. Interference fits are common on high-torque applications but require heat or hydraulic assistance to install.
Balance grade becomes critical above roughly 3,600 RPM. Below that, most standard couplings are fine. Above it, specify the balance grade and verify it, because an unbalanced coupling at speed will destroy bearings.
And don’t forget guarding. Rotating couplings injure people. MSHA inspectors will ask about it, and so will your insurance carrier.
DO THE MATH ON TOTAL COST, NOT PURCHASE PRICE
The purchase price of a coupling is almost irrelevant compared to what it costs when it fails. A coupling failure on a critical slurry pump might mean eight hours of lost production, a crew on overtime, and expedited freight on a replacement. Run that number, then compare it to the price difference between an adequate coupling and the right one.
Standardize where you can. Carrying three coupling types across the plant instead of twelve simplifies spares, training, and troubleshooting. But don’t standardize so aggressively that you force the wrong coupling into a demanding application just because it’s already on the shelf.
THE BOTTOM LINE
Selecting a flexible coupling for high-pressure mining duty comes down to honest answers about torque, misalignment, environment, vibration, and maintenance capability. Get those five things right and the coupling becomes the least interesting part of your drive train, which is exactly what you want.
If you’re specifying a new installation or chasing a repeat failure, bring in an application engineer early and give them real data: horsepower, speed, torque profile, misalignment tolerance, temperature range, contamination exposure, and duty cycle. The right coupling for your application exists. The work is in defining your application clearly enough to find it.